
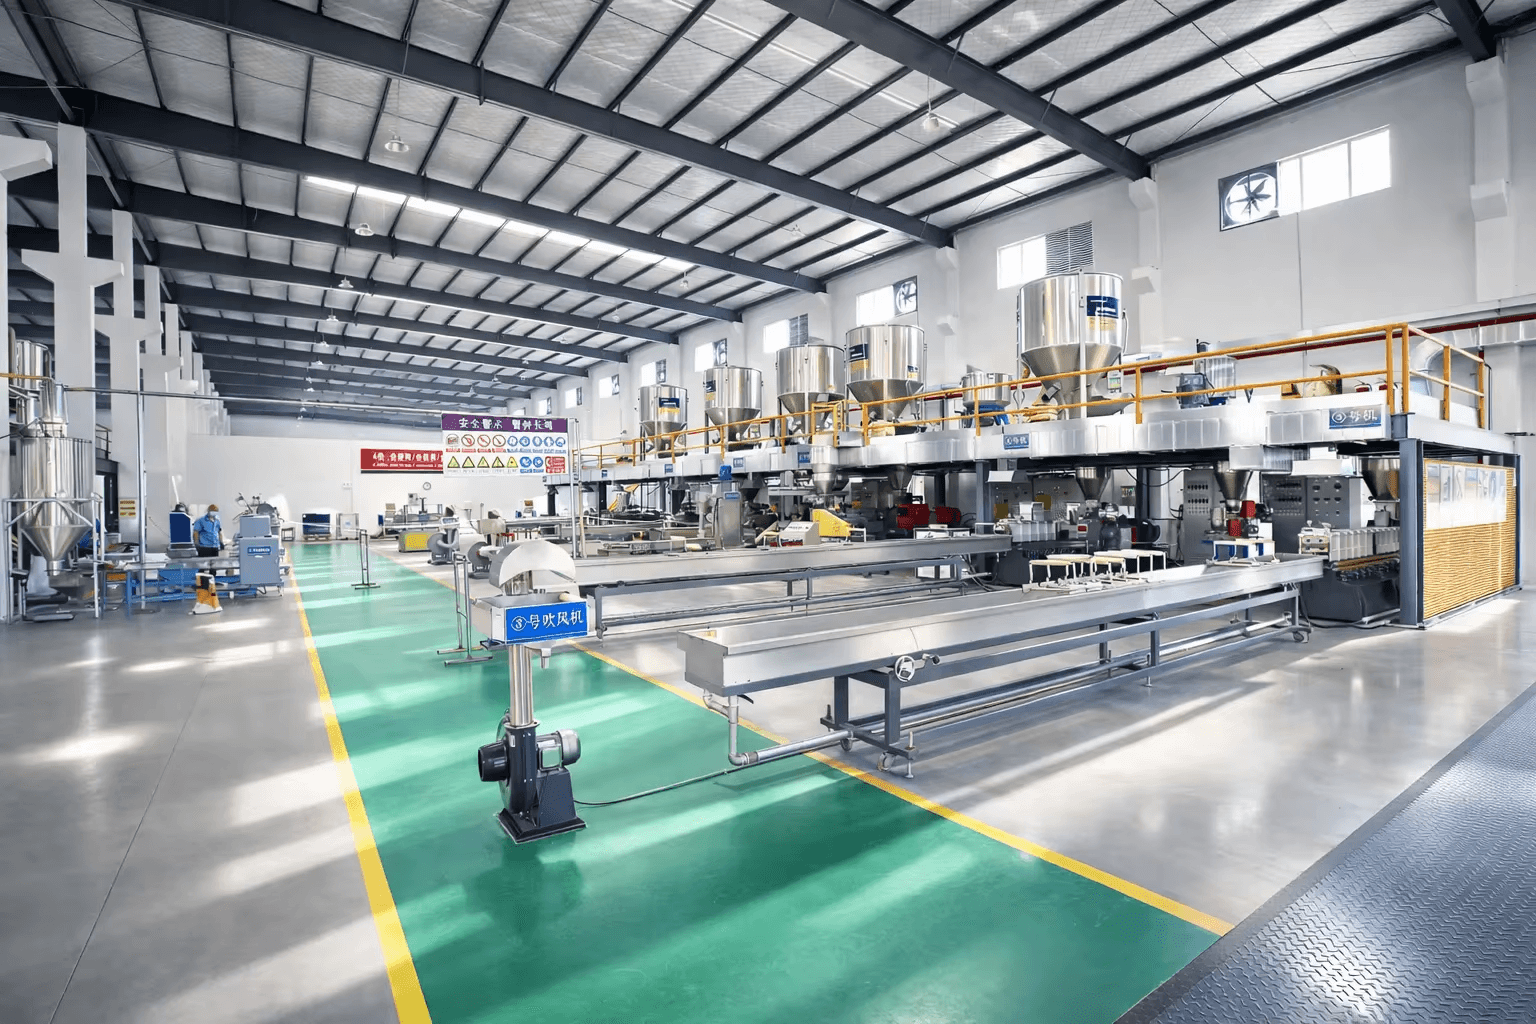
PA6 Grade Selection
Glass Fiber Reinforced PA6 Compounds
Explore 17 PLATFORM® PA6 grades from GF8 to GF50. Compare stiffness, impact and heat-deflection data for your molded part.
PA6 GF Compounds
GF8–GF50 across stiffness, impact, and heat deflectionGrade directory
PA6 glass-fiber grades
Grades are ordered by glass-fiber content. Compare the published properties, then open a grade or request its full TDS.
Full parameters & test methods
Scroll sideways to compare all properties →
| Grade / TDS | Glass fiber | Tensile stress | Flexural strength | Flexural modulus | Notched impact | HDT (1.8 MPa) | Water absorption |
|---|---|---|---|---|---|---|---|
| 8% | 77 MPa | 110 MPa | 3300 MPa | 7.5 kJ/m² | 190 °C | 1.45 % | |
| 15% | 120 MPa | 190 MPa | 5500 MPa | 7 kJ/m² | 205 °C | 1.3~1.7 % | |
| 15% | 120 MPa | 170 MPa | 5900 MPa | 8.5 kJ/m² | 200 °C | 1.3~1.7 % | |
| 15% | 110 MPa | 160 MPa | 4950 MPa | 9.5 kJ/m² | 195 °C | 1.3~1.7 % | |
| 20% | 125 MPa | 185 MPa | 6500 MPa | 5.5 kJ/m² | 205 °C | 1.4 % | |
| 20% | 140 MPa | 205 MPa | 6400 MPa | 8.5 kJ/m² | 210 °C | 1.3~1.7 % | |
| 30% | 185 MPa | 265 MPa | 8800 MPa | 13 kJ/m² | 210 °C | 1.1~1.5 % | |
| 30% | 160 MPa | 230 MPa | 8700 MPa | 7 kJ/m² | 210 °C | 1.25 % | |
| 30% | 165 MPa | 230 MPa | 8200 MPa | 10.5 kJ/m² | 210 °C | 1.25 % | |
| 30% | 180 MPa | 260 MPa | 9500 MPa | 11.5 kJ/m² | 210 °C | 1.25 % | |
| 32% | 190 MPa | 290 MPa | 9600 MPa | 15 kJ/m² | 210 °C | 1.1~1.5 % | |
| 35% | 195 MPa | 280 MPa | 10500 MPa | 13.5 kJ/m² | 210 °C | 1.1~1.5 % | |
| 40% | 155 MPa | 230 MPa | 9500 MPa | 17.5 kJ/m² | 205 °C | 0.8~1.2 % | |
| 40% | 210 MPa | 315 MPa | 13000 MPa | 13.5 kJ/m² | 205 °C | 0.8~1.2 % | |
| 45% | 225 MPa | 340 MPa | 13700 MPa | 18.5 kJ/m² | 210 °C | 0.8~1.2 % | |
| 45% | 200 MPa | 310 MPa | 13500 MPa | 15.5 kJ/m² | 210 °C | 0.8~1.2 % | |
| 50% | 230 MPa | 345 MPa | 14500 MPa | 17 kJ/m² | 210 °C | 0.8~1.2 % |
PA6 · Glass fiber 8%
EAG108U
- Density
- 1.15
- Tensile stress
- 77 MPa
- HDT (1.8 MPa)
- 190 °C
- Flammability
- HB
PA6 · Glass fiber 15%
EAG115
- Density
- 1.23
- Tensile stress
- 120 MPa
- HDT (1.8 MPa)
- 205 °C
- Flammability
- HB
PA6 · Glass fiber 15%
EAG115H
- Density
- 1.25
- Tensile stress
- 120 MPa
- HDT (1.8 MPa)
- 200 °C
- Flammability
- HB
PA6 · Glass fiber 15%
EAG115U
- Density
- 1.21
- Tensile stress
- 110 MPa
- HDT (1.8 MPa)
- 195 °C
- Flammability
- HB
PA6 · Glass fiber 20%
EAG120
- Density
- 1.29
- Tensile stress
- 125 MPa
- HDT (1.8 MPa)
- 205 °C
- Flammability
- HB
PA6 · Glass fiber 20%
EAG120U
- Density
- 1.28
- Tensile stress
- 140 MPa
- HDT (1.8 MPa)
- 210 °C
- Flammability
- HB
PA6 · Glass fiber 30%
EAG130
- Density
- 1.37
- Tensile stress
- 185 MPa
- HDT (1.8 MPa)
- 210 °C
- Flammability
- HB
PA6 · Glass fiber 30%
EAG130A
- Density
- 1.36
- Tensile stress
- 160 MPa
- HDT (1.8 MPa)
- 210 °C
- Flammability
- HB
PA6 · Glass fiber 30%
EAG130H
- Density
- 1.36
- Tensile stress
- 165 MPa
- HDT (1.8 MPa)
- 210 °C
- Flammability
- HB
PA6 · Glass fiber 30%
EAG130U
- Density
- 1.37
- Tensile stress
- 180 MPa
- HDT (1.8 MPa)
- 210 °C
- Flammability
- HB
PA6 · Glass fiber 32%
EAG132H
- Density
- 1.39
- Tensile stress
- 190 MPa
- HDT (1.8 MPa)
- 210 °C
- Flammability
- HB
PA6 · Glass fiber 35%
EAG135
- Density
- 1.41
- Tensile stress
- 195 MPa
- HDT (1.8 MPa)
- 210 °C
- Flammability
- HB
PA6 · Glass fiber 40%
EAG140
- Density
- 1.41
- Tensile stress
- 155 MPa
- HDT (1.8 MPa)
- 205 °C
- Flammability
- HB
PA6 · Glass fiber 40%
EAG140U
- Density
- 1.46
- Tensile stress
- 210 MPa
- HDT (1.8 MPa)
- 205 °C
- Flammability
- HB
PA6 · Glass fiber 45%
EAG145
- Density
- 1.52
- Tensile stress
- 225 MPa
- HDT (1.8 MPa)
- 210 °C
- Flammability
- HB
PA6 · Glass fiber 45%
EAG145A
- Density
- 1.52
- Tensile stress
- 200 MPa
- HDT (1.8 MPa)
- 210 °C
- Flammability
- HB
PA6 · Glass fiber 50%
EAG150U
- Density
- 1.58
- Tensile stress
- 230 MPa
- HDT (1.8 MPa)
- 210 °C
- Flammability
- HB
Comparison basis: GF content ISO 1172; tensile stress ISO 527; flexural properties ISO 178; notched Charpy impact at 23 °C ISO 179/1eA; HDT at 1.8 MPa ISO 75; water absorption at 23 °C and 50% RH ISO 62. These are typical web reference values. The catalog does not specify the dry or conditioned state of the mechanical data; confirm it in the grade-specific TDS before final selection.
Engineering Trade-offs
Reinforcement changes more than stiffness
Use GF content to narrow the PA6 range, then evaluate the complete molded system. Higher listed reinforcement does not automatically produce the better part.
Increasing glass-fiber content can support
Across an appropriate formulation and test basis, glass-fiber reinforcement is commonly screened when these requirements control the shortlist.
- Higher stiffness and load response
- Higher tensile and flexural strength
- Higher heat-deflection response
- Improved creep resistance
- Dimensional control under load
The same shortlist must also review
More fiber does not settle the material decision. The molded result remains sensitive to geometry, process, moisture state and the complete load path.
- Impact trade-offs and failure mode
- Fiber orientation and anisotropy
- Directional shrinkage and warpage
- Surface finish and exposed fibers
- Moisture conditioning and retained dimensions
- Weld lines, gates and local stress
Application Context
Connect the grade to the part architecture
Match the part's load, temperature and environment to a candidate grade before starting molding trials.
Before Final Selection
Validate moisture, molding and the actual part
PA6 absorbs moisture and its molded performance depends on conditioning, geometry and process history. Treat catalog values as screening inputs and close the decision on the intended tool and part.
- 01
Define the moisture state
Record whether the comparison uses as-molded, dry or conditioned specimens. Do not mix those states in one conclusion.
- 02
Control drying and material handling
Use grade-specific processing guidance and prevent uncontrolled moisture pickup before molding trials.
- 03
Review orientation and weld lines
Relate the gate, flow path and weld-line position to the real load direction and critical dimensions.
- 04
Measure shrinkage and warpage on the part
Catalog shrinkage data are not complete across this range. Measure the intended geometry instead of filling the gap with assumed values.
- 05
Run the intended tool and process window
Confirm filling, surface, dimensions, repeatability and local defects under production-relevant molding conditions.
- 06
Validate the assembled function
Close load, environment, cycling, assembly and customer evidence requirements before production approval.
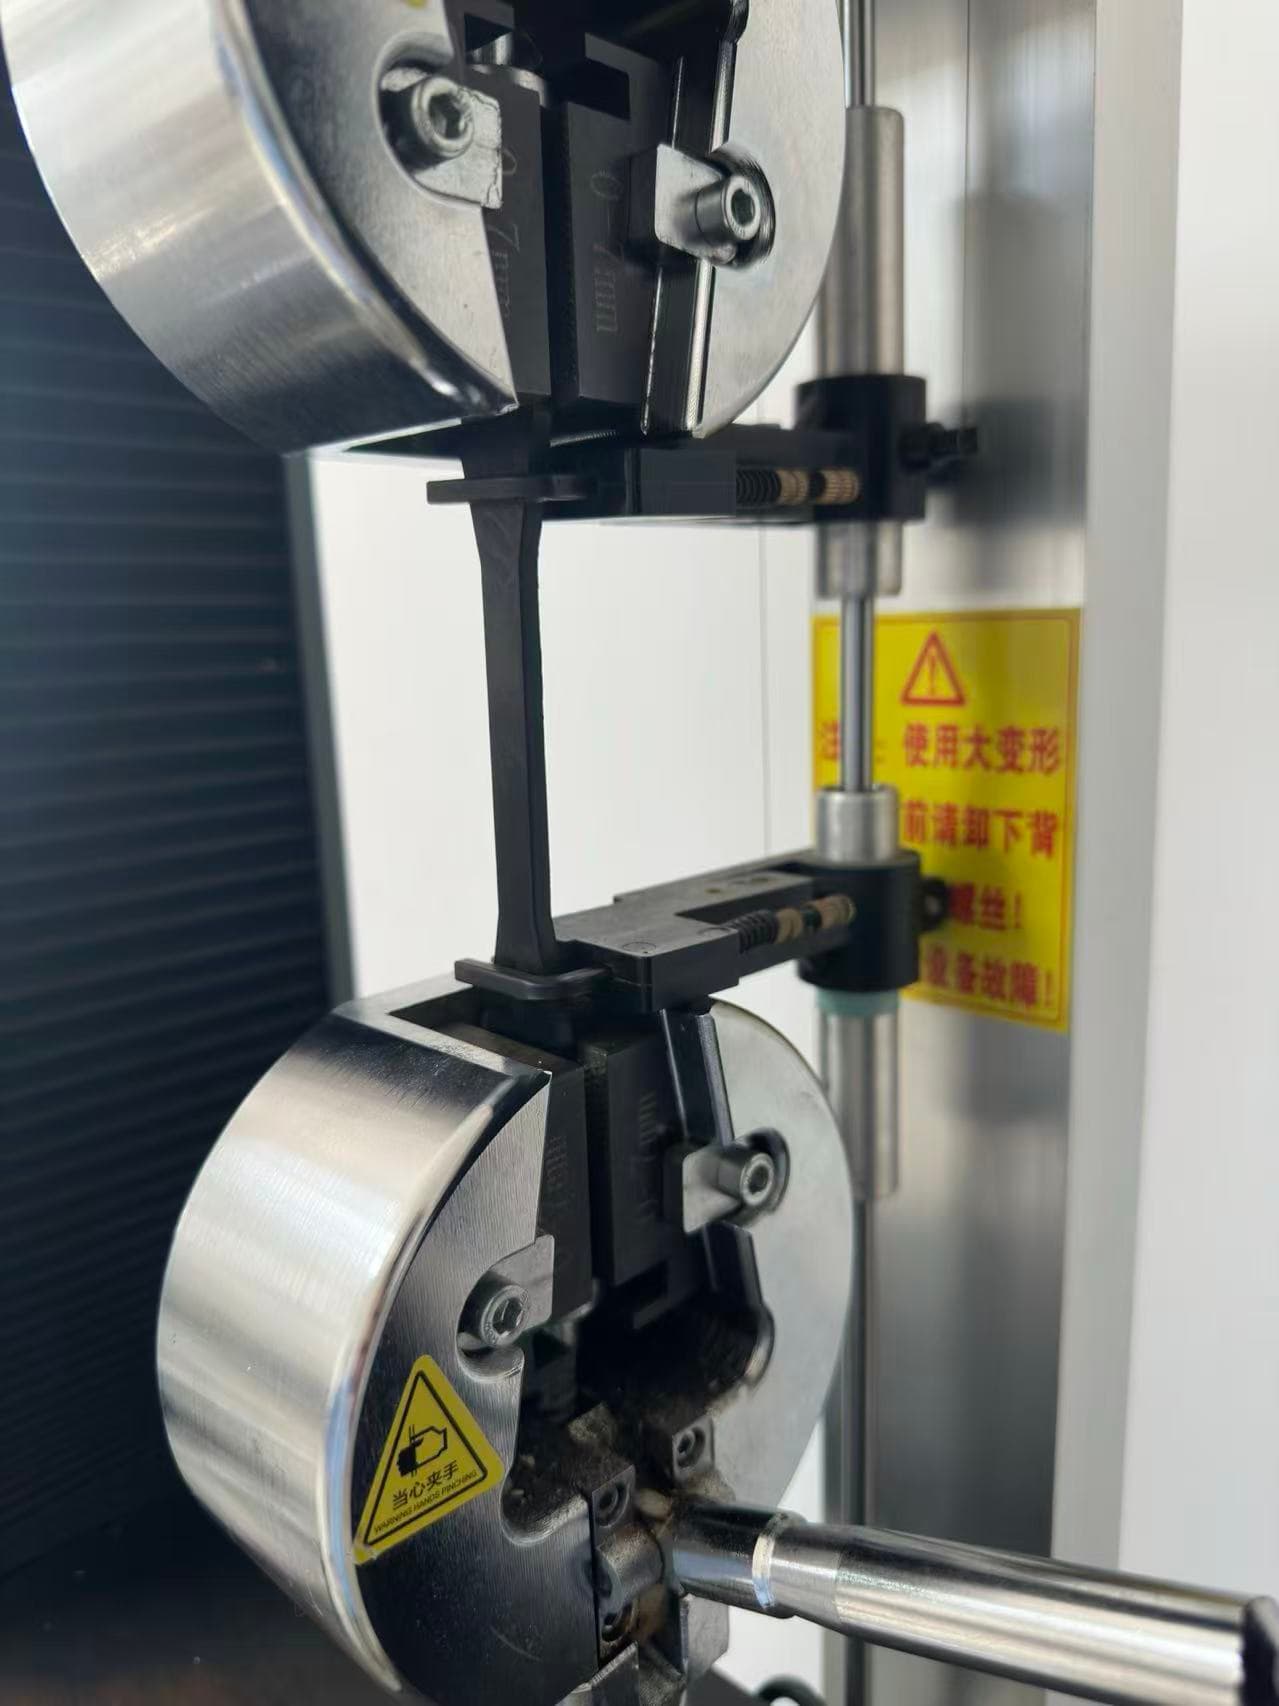
Project Inquiry
Move from PA6 GF screening to a molding decision
Share the part, current material, load, temperature, moisture state, mold stage, target properties and document requirements. Taiyi Polymer can help narrow the listed grades for project evaluation.
01Part & operating conditions
02Grade data & documents
03Molded-part validation